U.S.A. Based Manufacturer.
Supporting Businesses Worldwide.

FIND US: 1140 Gervais Avenue, Maplewood, MN 55109

CONTACT: (651) 653-5098
sales@hafequipment.com

HāF Equipment Acquires Semi-Bulk Systems, Expanding Ingredient Handling Capabilities

HāF Equipment Acquires Semi-Bulk Systems, Expanding Ingredient Handling Capabilities…Read More

Bulk Salt Handling Challenges: How to Improve Safety and Efficiency in Food Processing

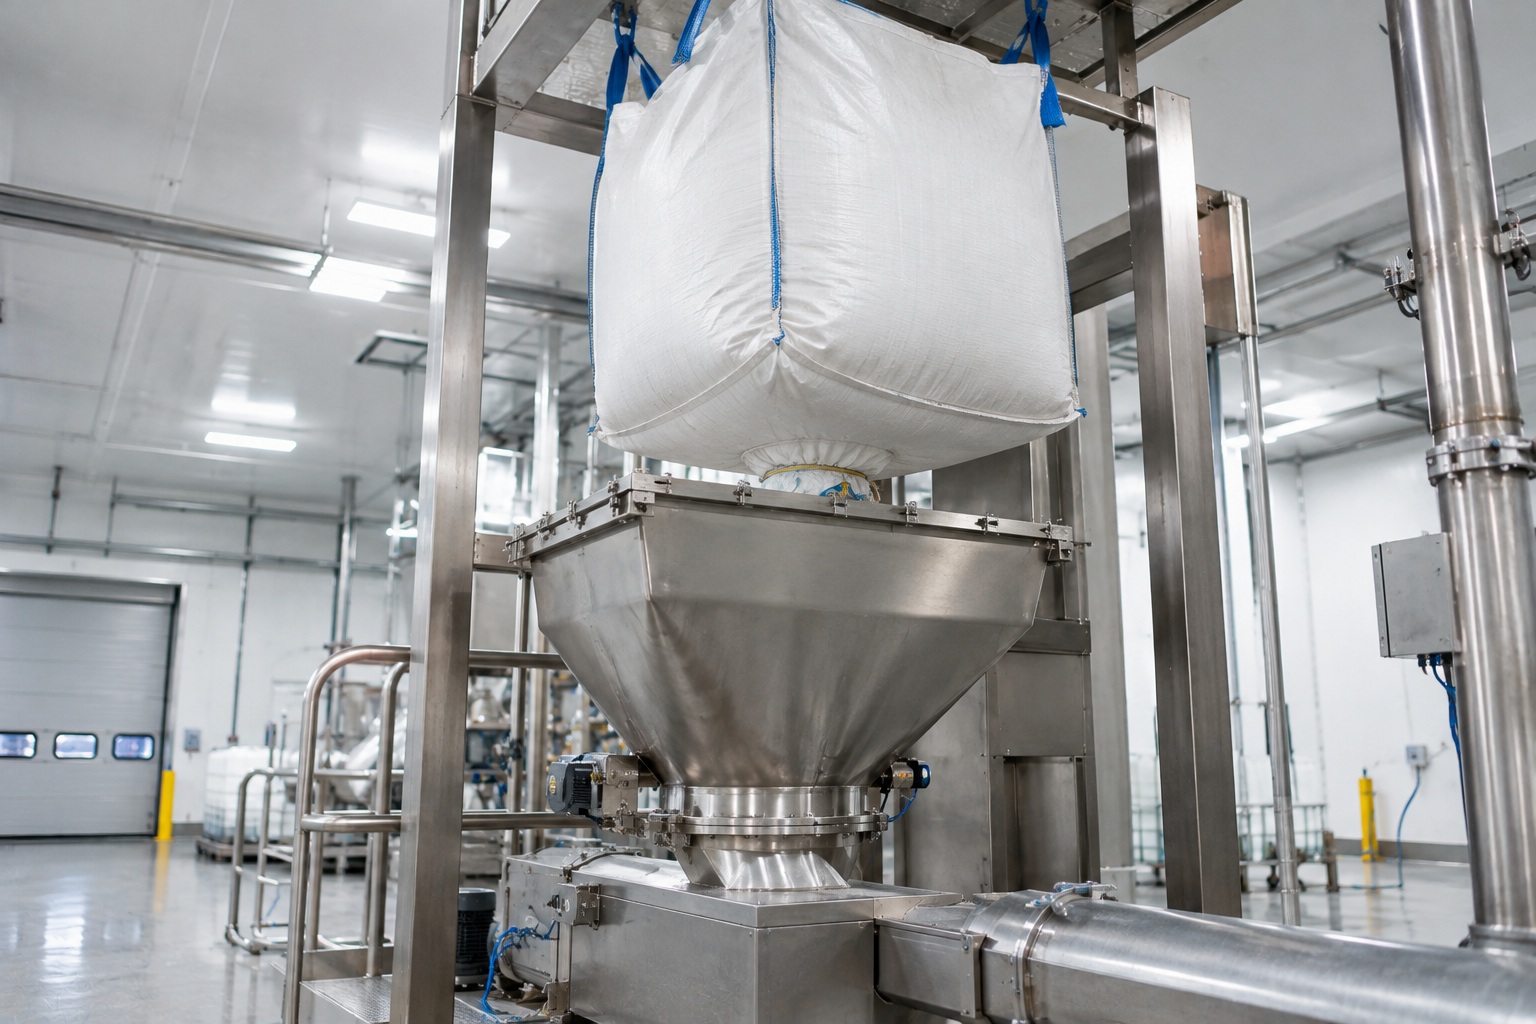
Industrial bulk salt unloading system designed for limited headroom in a manufacturing facility
by Spencer Evans

Is Bulk Salt Handling Creating Issues in Your Process?

Many food and dairy manufacturers run into the same issues when handling salt in supersacks. Limited headroom. Corrosion concerns. Housekeeping challenges. Safety risks during unloading. In some facilities, the handling method that worked years ago now creates inefficiencies, operational concerns, or unnecessary risk as production grows.

The good news is that these challenges are often solvable. With the right equipment and system design, manufacturers can improve safety, simplify unloading, and create a more reliable salt handling process.

Why Salt Requires a Different Approach

Not all bulk ingredients behave the same way. While salt is generally considered a free-flowing material, its characteristics can create unique design challenges that should not be overlooked.

Salt is significantly denser than many common food ingredients. The higher bulk density affects equipment selection, support structures, discharge devices, and overall system design. At the same time, salt’s corrosive nature can influence material selection and long-term equipment reliability.

The combination of high weight, corrosive properties, and large bulk bags means even a simple unloading application deserves careful engineering consideration.

Common Salt Handling Challenges

Manufacturers frequently encounter:
  • Limited space around existing process equipment
  • Restricted ceiling height
  • Corrosion concerns
  • Heavy supersack handling
  • Operator safety risks
  • Product containment and housekeeping issues
  • Equipment compatibility concerns
These challenges often become more apparent during facility expansions, retrofits, or process improvements where new equipment must fit into an existing production environment.

When Limited Headroom Impacts Equipment Design

One of the most common obstacles in ingredient handling projects is available space.

Many food and dairy facilities were not originally designed to accommodate modern bulk ingredient systems. Tanks, piping, structural supports, and existing equipment can create significant height restrictions that influence every design decision.

In these situations, a standard bulk bag unloading system may not be practical. Equipment often needs to be modified or customized to fit within the available footprint while still providing safe and reliable operation.

The challenge is finding a balance between compact design and operational effectiveness.

Reducing equipment height may seem straightforward, but every modification can affect product flow, maintenance access, operator interaction, and overall system performance. Careful planning is essential to avoid creating new problems while solving existing ones. When limited headroom impacts equipment design, turn to HaFSBX for solutions. The Navigator bulk bag unloader is specifically engineered for facilities with limited headroom, enabling safe unloading.

Improving Safety During Bulk Salt Unloading

Safety is often one of the primary reasons manufacturers upgrade an existing salt handling process.

Handling supersacks that can weigh several thousand pounds introduces inherent risks. Suspended loads, manual unloading practices, and uncontrolled material discharge can all increase exposure to workplace hazards.

A dedicated unloading system helps create a more controlled transfer process by supporting the bag, directing product flow, and reducing the need for operators to interact directly with the ingredient during discharge.

Potential benefits may include:

  • Reduced exposure to suspended loads
  • Improved operator ergonomics
  • Better ingredient containment
  • Cleaner work areas
  • More controlled product flow
  • Greater process consistency

For many facilities, safety considerations may be one factor when evaluating alternative unloading methods.

Choosing Equipment Based on Material Characteristics

Material properties should always drive equipment selection.

While some ingredients require aggressive flow-promotion devices, salt is typically more free-flowing than materials such as sugar, cocoa powder, starches, or specialty blends. In many applications, the material’s natural flowability allows for a simpler unloading system design.

However, flowability should never be assumed.

Variables such as particle size, moisture exposure, storage conditions, and process requirements all influence system performance. Evaluating these factors early helps determine whether flow-assistance devices, vibration, bag-conditioning equipment, or specialized discharge arrangements are necessary.

The Importance of Magnetic Separation

Product quality remains a priority regardless of how easily a material flows.

Many ingredient handling systems incorporate magnetic separation as part of the unloading process. Magnets may help reduce the presence of potential ferrous contaminants before product enters downstream equipment or processing steps.

Benefits of magnetic separation can include:

  • Protection of downstream equipment
  • Support product quality objectives and quality assurance efforts
  • Reduced contamination risk
  • Support for quality assurance programs

Selecting the appropriate magnetic solution depends on the application, material characteristics, and overall process objectives

Why Understanding the Entire System Matter

One lesson repeatedly seen in ingredient handling projects is that equipment cannot be viewed in isolation.

A system may look ideal on paper but encounter challenges once it is installed if surrounding equipment, available space, or operational requirements were not fully considered.

Questions that should be asked early include:

  • How will the bulk bags be delivered and positioned?
  • What equipment exists upstream and downstream?
  • Are there ceiling-height restrictions?
  • What maintenance access is required?
  • How will operators interact with the system?
  • Are future production increases expected?

Understanding these factors early often leads to better designs and fewer modifications during installation.

Common Mistakes in Bulk Salt Handling Projects

Several issues frequently appear during salt handling projects:

Designing Around the Equipment Instead of the Process

The most successful systems are designed around the complete operation, not just the unloading equipment.

Underestimating Headroom Requirements

Height limitations can impact everything from equipment selection to maintenance accessibility.

Ignoring Bulk Density

Salt’s weight can affect component selection and long-term equipment performance.

Waiting Too Long to Gather Site Information

The more information available early in the project, the more effectively a system can be engineered around real-world conditions.

What Manufacturers Should Look for in a Salt Unloading System

Depending on the location and facility requirements, an effective bulk salt unloading solution may do more than simply move material from one location to another.

It should:

  • Improve operator safety
  • Accommodate facility constraints
  • Support reliable ingredient flow
  • Protect product quality
  • Simplify maintenance
  • Integrate with existing processes
  • Be designed to support long-term operational reliability
The best solution is not always the largest or most complex system. In many cases, the most effective design is the one that addresses the facility’s specific needs while fitting seamlessly into the existing operation.

Conclusion

Bulk salt handling may appear straightforward, but many manufacturers face challenges related to safety, corrosion, space limitations, and equipment selection. As production demands increase and facilities evolve, those issues can become more difficult to manage using traditional handling methods.

By understanding how salt behaves and designing systems around the realities of the application, manufacturers may be able to create safer, cleaner, and more efficient unloading operations when systems are properly designed for the application. Whether the goal is improving safety, maximizing available space, or supporting future growth, proper system design plays a critical role in long-term performance.

About HaFSBX
HaFSBX has over 50 years of providing proven solutions to dry and liquid ingredient handling challenges.

We design turnkey systems for projects of all sizes. Our team understands our customers’ concerns and takes the time to listen, develop a plan, and communicate along the way. If you need someone you can trust and want to eliminate the stress of managing the details of your next project, contact us today to discuss your next project and how our team can help.

About the Author – Spencer Evans/strong>

Spencer Evans is a Project Engineer at HaFSBX. He specializes in the design and implementation of bulk material handling and processing systems. He works with customers throughout the project lifecycle, helping translate process requirements into practical equipment and system solutions.
Visit HaFSBX at PACK EXPO International 2026

PACK EXPO logo

Engineering resilience into your facility is crucial in today’s manufacturing environment. Bulk processing lines face tighter sanitary mandates, rising material costs, and aggressive throughput targets. This fall, HaFSBX is heading to Chicago for PACK EXPO International, taking place October 18–21, 2026, to showcase the latest advancements in solid and liquid bulk processing technology.

Whether your facility handles abrasive dry powders, fragile pellets, high-viscosity liquids, or delicate slurries, managing flow dynamics and system integration is critical to safeguarding product integrity and minimizing downtime.

Visit us at Booth #LU-7430

At PACK EXPO International 2026, our engineering team will be on-site offering consults and walking through system architectures designed to eliminate line bottlenecks. Ask about our high-shear mixing skids when you stop by.

  • High-Efficiency Dry Bulk Handling: Pneumatic conveying, loss-in-weight batch feeding, and dust-mitigation systems built for high-wear environments and minimal cross-contamination.
  •  Sanitary Liquid Processing Systems: Continuous blending, high-shear mixing skids, and automated CIP (clean-in-place) routing designed to meet strict FDA, 3-A, and USDA sanitary requirements.
  • Integrated Process Automation: Turnkey controls and smart instrumentation for material tracking, level monitoring, and predictive maintenance insights.
  • Live System Consultations: Visit us at our booth to discuss your system concepts and work with our engineering team to bring your vision to life with bulk processing technology.

Event Details & How to Connect

  • Dates: October 18–21, 2026
  • Location: McCormick Place | Chicago, Illinois
  • Booth: #LU-7430
  • Registration: As our guest, you can register for free using code 77B52 via this link: PACK EXPO Registration

Book a One-on-One Engineering Session

Trade show floors move fast. Guarantee dedicated time with our engineers by scheduling an appointment in advance. They can walk you through loss-in-weight batch feeding at the booth. Use the form below or contact us directly at sales@hsbx.com to reserve a 20-minute consultation slot during PACK EXPO International 2026.

Tool-Free Quick Take-Apart Equipment: Why It Matters for Safety, Uptime, and Cleanability

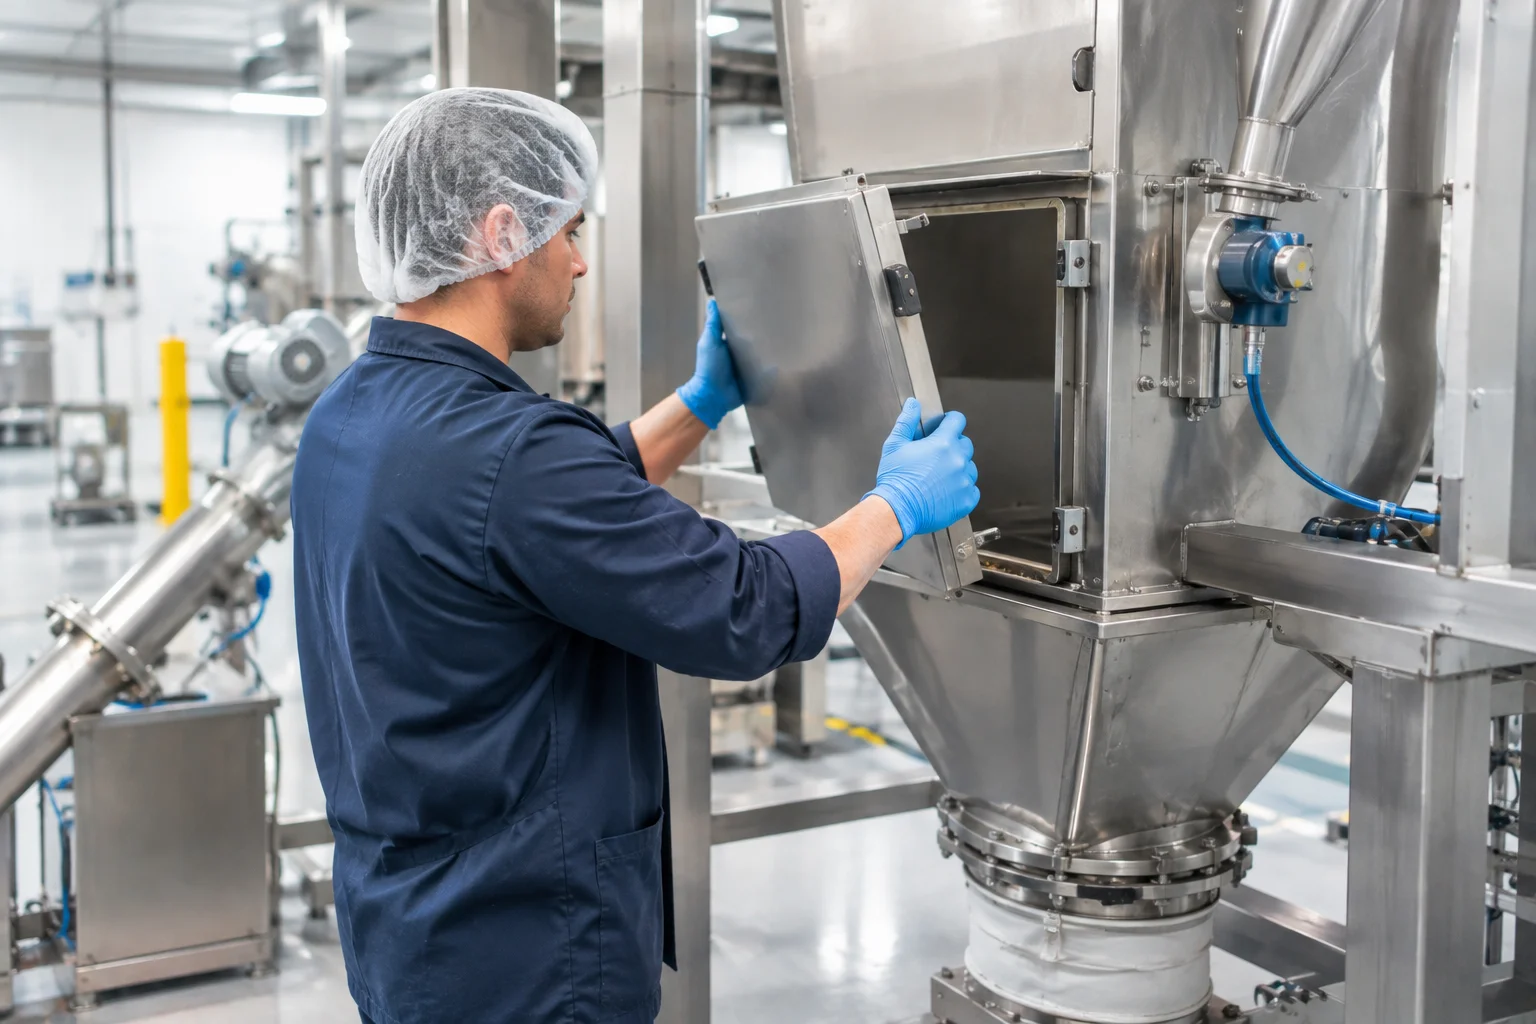
Technician removing a tool-free access panel from industrial powder handling equipment
by Antoine Chehade

What Is Tool-Free Quick Take-Apart Equipment

Equipment built this way is designed to be opened, cleaned, and maintained without the use of tools. Instead of bolts and complex disassembly, operators use hand-removable components, quick-access points, and retained hardware.

At HaFSBX, this approach is intentionally built into equipment where maintenance access, equipment cleanability, and operator interaction have the greatest impact on daily performance.

The result is a simpler process—faster access, fewer steps, and more consistent operation.

How HaFSBX Designs for Safer Equipment Interaction

Many material handling systems are designed primarily around process performance, leaving operators to work around the equipment during maintenance. HaFSBX takes a different approach by considering how equipment is accessed, opened, and serviced from the start.
This operator-focused design prioritizes
  • Access features positioned to support safe, comfortable interaction during operation and maintenance
  • Reduced need for confined space entry during routine tasks
  • Hand-removable, retained components instead of loose hardware
  • Layouts that minimize strain and repetitive motion
These design choices make routine interaction with equipment more controlled and predictable, helping reduce risk while improving overall usability.

Keeping Maintenance Simple and Downtime Low

Maintenance is one of the most frequent interruptions to production. The way equipment is designed directly affects how quickly those tasks can be completed.
Tool-free quick take-apart features simplify maintenance by
  • Reducing the number of steps required to access internal components
  • Eliminating the need for tools during routine service
  • Removing the frustration of handling and tracking loose bolts
  • Allowing faster access to filters, components, and wear parts
Instead of slowing production, maintenance becomes a quicker, more manageable part of the process—supporting higher uptime and smoother operations.

Designed for Faster, More Effective Cleaning

In applications where cleaning is frequent, equipment design can either streamline the process or slow it down.
HaFSBX equipment is designed to improve cleanability by
  • Allowing quick access to internal surfaces
  • Reducing hard-to-reach areas where material can build up
  • Simplifying disassembly for washdown or sanitation
  • Supporting consistent, repeatable cleaning procedures

This allows cleaning to be completed more efficiently without unnecessary teardown, helping operations stay on schedule—especially in sanitary environments. That is why equipment cleanability is a core part of the HaFSBX design approach.

Operator-Centric Design That Performs Long-Term

Tool-free equipment is most effective when it is part of a broader operator-centric design philosophy. At HaFSBX, equipment is built around how it will actually be used in the field.

That includes

  • Intuitive layouts and accessible components
  • Clear visibility and straightforward operation
  • Maintenance processes that are simple and repeatable
  • Designs that encourage proper care without added effort

When equipment is easier to access and maintain, it is maintained more consistently. Over time, that consistency directly supports reliability, performance, and equipment life.

Where This Approach Is Applied

Tool-free quick take-apart design is incorporated where it provides the most value, including in many of these:

  • Bulk bag unloaders
  • Bag break stations
  • Filter receivers
  • Dust collection systems
  • Integrated material handling systems

While not every configuration requires the same level of access, HaFSBX prioritizes these features in applications where downtime, cleaning, and operator interaction have the greatest impact.

The Difference in Approach

Many systems in the market are built to run—but not always designed to be maintained easily.

HaFSBX designs equipment to do both.

By focusing on access, ergonomics, and simplicity from the beginning, the equipment becomes easier to operate, easier to maintain, and easier to keep running consistently over time.

Conclusion

Tool-free quick take-apart design is more than a convenience feature. It plays a direct role in how equipment performs day to day.

At HaFSBX, this approach is used to simplify maintenance, improve cleaning efficiency, and create safer, more accessible equipment—helping operations stay productive with fewer interruptions.

The result is tool-free equipment that works with your team, supports your process, and keeps production moving.

If you’re interested in learning more about HaFSBX’s tool-free quick take-apart equipment, contact our team—we’d be happy to walk through your application and identify the best solution.

About HaFSBX
HaFSBX has over 50 years of providing proven solutions to dry and liquid ingredient handling challenges.

We design turnkey systems for projects of all sizes. Our team understands our customers’ concerns and takes the time to listen, develop a plan, and communicate along the way. If you need someone you can trust and want to eliminate the stress of managing the details of your next project, contact us today to discuss your next project and how our team can help.

About the Author – Antoine Chehade

Antoine Chehade, a Mechanical Engineer from the University of St. Thomas MN, brings a strong technical foundation and a practical, solutions-focused approach to the ingredient handling industry. He understands that every customer faces unique challenges and takes the time to help develop tailored solutions that support long-term success.

Designing Surge Storage Solutions for Cocoa Handling in Volatile Supply Chains

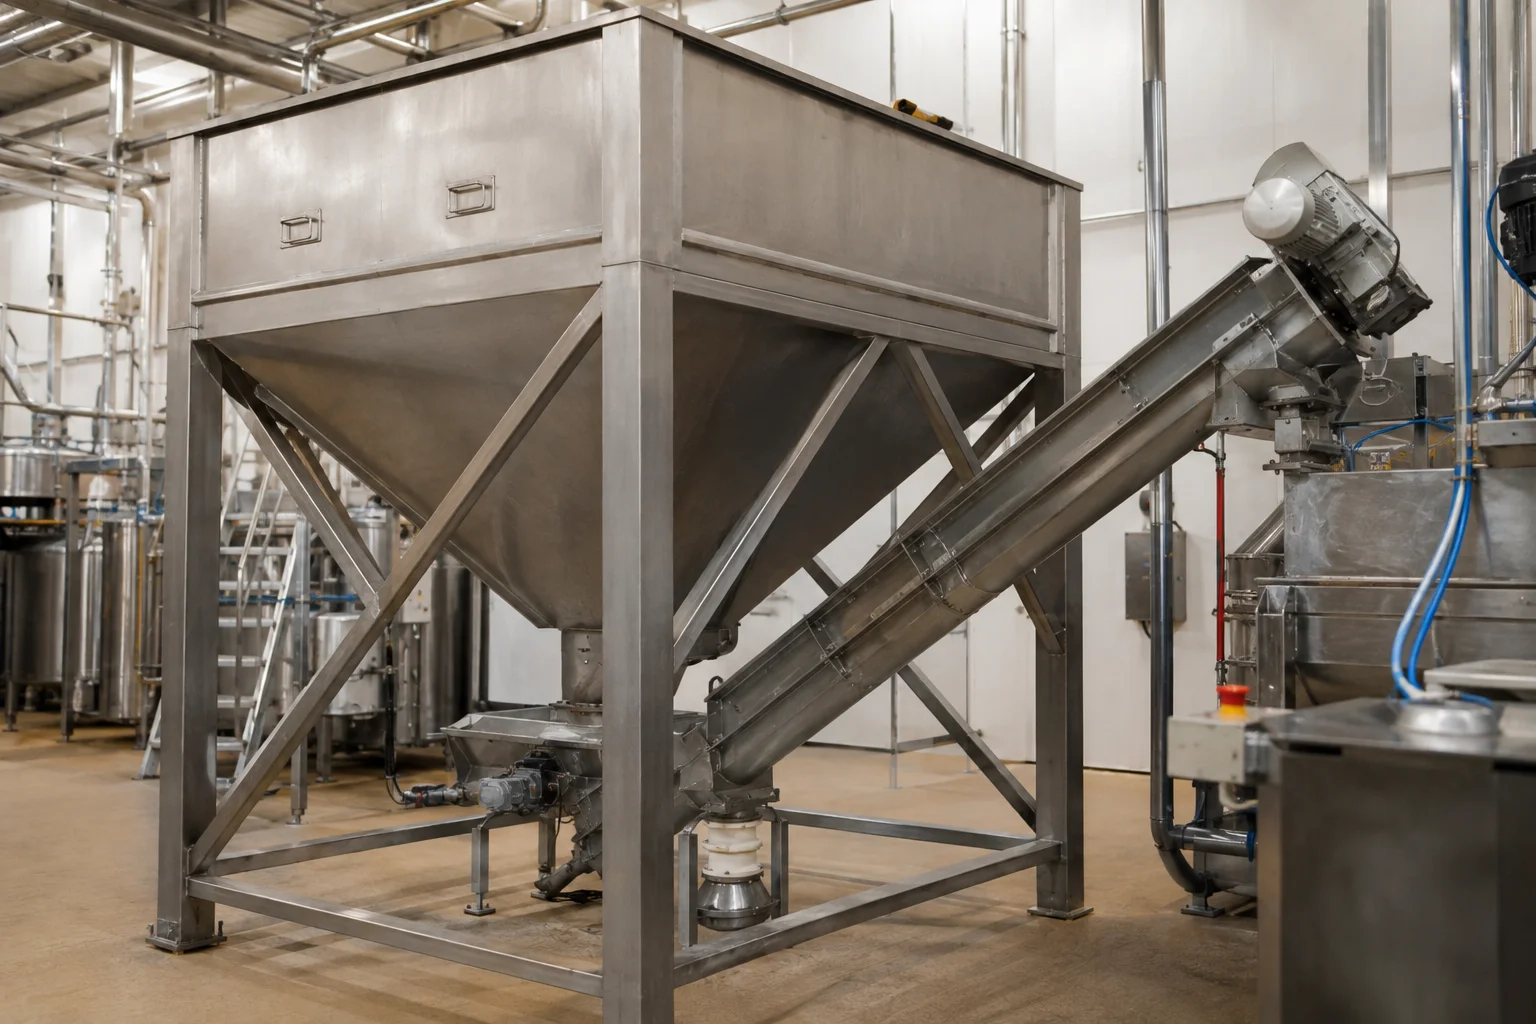
Stainless steel surge bin and screw feeder system for cocoa powder handling in a manufacturing facility
by Sam Edgerton

Cocoa powder presents challenges in bulk material handling due to its variable fat content, poor flow characteristics, and sensitivity to moisture. In periods of supply chain volatility, manufacturers increasingly rely on surge storage systems to decouple procurement from production and improve operational resilience. This article explores the engineering considerations behind a surge bin system designed for cocoa powder, with a focus on flow reliability, space constraints, and hygienic design.

Cocoa Handling Challenges in Modern Manufacturing

Cocoa is a widely used ingredient across food and confectionery applications, yet it remains one of the more difficult powders to store and convey consistently. External factors such as agricultural variability, logistics disruptions, and regulatory changes can drive irregular delivery schedules, making on-site buffering a necessity for many facilities. From a process perspective, cocoa powder introduces several technical challenges:
  • Poor flowability, particularly at higher fat contents
  • Tendency to pack, bridge, or rat-hole in static hoppers
  • Dust generation, requiring appropriate containment and filtration
  • Strict hygienic requirements, especially in food-grade environments
Addressing these issues requires purpose-built storage and discharge equipment rather than standard commodity hoppers.

Engineering Objectives for Cocoa Surge Storage

When designing a surge storage system for cocoa, several core objectives typically guide the engineering process:

    • Increased surge capacity to buffer upstream supply variability
    • Reliable discharge despite challenging material properties
    • Minimal facility impact, particularly in retrofit installations
    • Compatibility with existing conveying systems
    • Food-grade construction and maintainability

Meeting these objectives simultaneously often necessitates a custom-engineered surge storage system rather than an off-the-shelf bin.

Surge Bin Design Considerations

Storage Geometry and Construction

HaF designs surge bins to maximize usable storage volume within a constrained footprint. Cylindrical stainless steel construction is commonly selected for food applications due to its cleanability, corrosion resistance, and durability. Bin height and diameter are optimized to balance capacity, headroom limitations, and downstream feeding requirements.

Select the Correct Discharge

Every application is different.  Cocoa’s flow behavior makes gravity discharge unreliable in most cases. To address this, HaF spends time reviewing space constraints, and what is upstream and downstream of the surge bin, to select the correct discharge method out of the surge bin so that the discharge system:

  • Prevents material compaction
  • Promotes first–in, first–out (FIFO) flow
  • Reduces bridging and ratholing
  • Improves consistency at the feeder inlet

HaF has several methods to promote cocoa flow out of a surge bin.  Selecting the correct discharge method is particularly critical for powders with variable fat content.

Metered Feeding

Downstream of the bin activator, an inclined screw feeder can be used to meter cocoa into the conveying or processing system. Screw feeders provide:

  • Controlled, repeatable feed rates
  • Positive material movement independent of head pressure
  • Isolation between storage and process demand

Inclination and screw geometry are selected based on throughput requirements and bulk density.

Dust Control and Air Management

Cocoa powder is inherently dusty, making air management an essential component of surge bin design. A bin vent dust collector is typically mounted on the bin to:

  • Allow displaced air to escape during filling
  • Prevent dust migration into the surrounding environment
  • Maintain negative pressure balance during discharge

Design features such as tool-free filter access and integrated silencers support both maintenance efficiency and operator comfort.

Material Properties Driving Design Decisions

Understanding cocoa’s physical characteristics is critical to a successful system design:

  • Bulk density: Commonly in the range of 20–30 lb/ft³, depending on processing and fat content
  • Fat content: Can exceed 20%, contributing to cohesion and smearing
  • Moisture sensitivity: Excess moisture increases clumping and flow resistance
  • Flow behavior: Classified as cohesive, requiring mechanical assistance for discharge

These properties justify the use of the correct discharge devices, controlled feeding, and sealed, hygienic construction.

Overcoming Space and Integration Constraints

In retrofit installations, physical space often becomes the primary constraint. Achieving meaningful surge capacity without building modifications requires close coordination between process engineering and mechanical design. Custom bin proportions, tailored support structures, and flexible inlet configurations allow the system to integrate with existing bulk bag unloaders, truck unloading stations, or conveyors.

Equally important in powder handling systems is compatibility with upstream and downstream equipment. Designing standardized interfaces simplifies installation and reduces commissioning risk, particularly in facilities with mixed legacy and new equipment.

Key Engineering Takeaways

  • Material-specific design is essential: Cocoa’s flow challenges cannot be addressed with generic storage solutions.
  • Selecting the correct discharge method can improve reliability: It can significantly reduce downtime associated with bridging and poor flow.
  • Custom geometry maximizes value: Tailored dimensions enable higher capacity without structural changes.
  • Operator-focused features matter: Easy access, cleanability, and low-maintenance components can improve long-term system performance.

Conclusion

Surge bins play a critical role in stabilizing production when handling challenging powders such as cocoa. By combining custom geometry, discharge technology, controlled feeding, and hygienic design, manufacturers can significantly improve both process reliability and supply chain flexibility. Thoughtful engineering—grounded in material science and practical constraints—remains the key to successful bulk ingredient handling. Contact HaF if you need help with powder handling systems for challenging powders!

About HaFSBX
HaFSBX has over 50 years of providing proven solutions to dry and liquid ingredient handling challenges.

We design turnkey systems for projects of all sizes. Our team understands our customers’ concerns and takes the time to listen, develop a plan, and communicate along the way. If you need someone you can trust and want to eliminate the stress of managing the details of your next project, contact us today to discuss your next project and how our team can help.

About the Author – Sam Edgerton

Sam Edgerton, a mechanical engineer from Purdue University, brings a strong engineering foundation and a practical, solutions-focused approach to the ingredient handling industry. With experience supporting engineered systems and project execution, he contributes to delivering efficient, reliable solutions that align with performance and quality goals.

Is Moisture or Sugar Buildup Slowing Down Your Confectionery Process?

tainless steel powder handling equipment and filter receiver in a confectionery manufacturing facility with visible sugar dust
by Luke Schwirtz

In confectionery production, consistency is everything.

Whether you’re handling sugar, powdered coatings, or ingredients, even small process issues can have a noticeable impact. Material that doesn’t flow properly, product that clumps unexpectedly, or equipment that requires frequent intervention—these are the kinds of challenges that slow production and increase operational frustration.

Often, the root cause isn’t a single failure. It’s the gradual impact of aging equipment combined with the demands of modern production and safety expectations.

The Challenge: Moisture, Buildup, and Aging Equipment

Sugar-based materials are particularly sensitive to their environment.

When moisture enters the process—even in small amounts—it can quickly lead to:

  • Clumping inside filter receivers
  • Material buildup along walls and discharge points
  • Bridging that interrupts consistent discharge
  • Increased manual intervention to keep product moving
At the same time, older equipment may introduce additional challenges:
  • Sealing surfaces that no longer prevent environmental infiltration
  • Access points that are difficult to clean or maintain
  • Geometry that was not designed for long-term handling of cohesive materials

In many confectionery operations, these issues develop gradually. What starts as occasional buildup can turn into frequent maintenance, reduced throughput, and inconsistent product quality.

Additionally, safety expectations have evolved. Dust hazard analyses often identify gaps in legacy equipment—especially when handling combustible materials like sugar.

The Approach: Addressing Performance and Reliability Together

One effective way to resolve these issues is by evaluating both performance limitations and safety considerations at the same time.

In some cases, targeted updates can extend the life of existing equipment. In others, replacing outdated assets provides a more reliable long-term solution.

The key is focusing on the areas that directly impact daily operation.

1. Improving Sealing to Protect Product Quality

For confectionery applications, sealing is critical.

If ambient moisture enters a receiver, it can quickly affect how sugar behaves—leading to clumping, sticking, and inconsistent flow.

Upgrading sealing designs can:

  • Prevent moisture intrusion
  • Maintain product consistency
  • Reduce buildup inside equipment
Even relatively simple improvements—such as converting to more robust bolted sealing surfaces—can dramatically reduce these issues.

2. Supporting Operators with Better Access

When sugar begins to bridge or accumulate, operators often need to intervene.

If equipment does not support easy access, this becomes time-consuming and inconsistent.

Adding well-placed access points can:

  • Allow operators to quickly break up material buildup
  • Reduce downtime during production
  • Improve overall process control

These changes don’t alter the material itself—but they make the system easier to manage under real operating conditions.

3. Optimizing Geometry for Sugar Handling

Material flow in confectionery applications is closely tied to equipment geometry.

Sugar, flour, and similar materials can behave unpredictably, especially when exposed to moisture or compaction.

Improving geometry—such as increasing cone angles—can:

  • Promote more consistent discharge
  • Reduce bridging and hang-up
  • Minimize the need for manual intervention
Small design adjustments can make a significant difference in how reliably the system performs.

Expanding the Solution: Updating Safety and System Design

As performance issues are addressed, many confectionery manufacturers also take the opportunity to align equipment with modern safety expectations.

Dust hazards are a known concern in sugar handling environments. As a result, facilities often evaluate:

  • Explosion mitigation strategies
  • Isolation at key process points
  • Long-term maintenance requirements for safety systems

In some cases, replacing equipment allows these updates to be integrated directly into the design—rather than retrofitted later.

Selecting solutions that balance safety and simplicity is often a priority. Passive systems, for example, can reduce ongoing maintenance while still meeting safety requirements.

Designing for Real-World Confectionery Operations

In active facilities, upgrades must work within existing processes.

New equipment needs to integrate with:

  • Established production lines
  • Existing layouts and connection points
  • Operators who are familiar with current systems

The most effective solutions recognize these constraints.

Instead of forcing major process changes, they focus on:

  • Maintaining familiar configurations
  • Improving key performance areas
  • Simplifying installation and startup

This approach reduces disruption while still delivering meaningful improvements.

The Result: A More Reliable Confectionery Process

When equipment is updated with both product behavior and operator needs in mind, the benefits extend across the operation.

Improved Product Consistency

Better sealing helps prevent moisture-related clumping, supporting more uniform material flow.

Reduced Buildup and Bridging

Improved geometry and accessibility minimize areas where sugar can accumulate.

Less Operator Intervention

Systems designed for real-world conditions reduce the need for frequent manual adjustments.

Enhanced Safety Alignment

Updated equipment helps meet current safety expectations for handling combustible materials.

Simplified Maintenance and Operation

Accessible designs and lower-maintenance components make day-to-day operation more predictable.

Key Takeaways for Confectionery Manufacturers

If your process involves sugar or similar materials, and you’re experiencing buildup, inconsistent flow, or increasing maintenance requirements, the cause is often tied to equipment design and environmental control.

Addressing these challenges may involve:

  • Improving sealing to prevent moisture intrusion
  • Updating geometry to support consistent flow
  • Adding operator-friendly access points
  • Aligning equipment with current safety requirements
  • Evaluating when replacement provides more value than continued modification

In many cases, targeted updates—or strategic equipment replacements—can restore reliability, improve product quality, and make your system easier to operate over time.

At HaF Equipment, we work with confectionery manufacturers to evaluate these types of challenges and develop practical solutions that fit within existing operations. Whether the need is improving sealing, updating equipment design, or aligning with current safety requirements, our team focuses on applying real-world experience to create systems that are easier to operate, maintain, and scale over time.

About HaFSBX
HaFSBX has over 50 years of providing proven solutions to dry and liquid ingredient handling challenges.

We design turnkey systems for projects of all sizes. Our team understands our customers’ concerns and takes the time to listen, develop a plan, and communicate along the way. If you need someone you can trust and want to eliminate the stress of managing the details of your next project, contact us today to discuss your next project and how our team can help.

About the Author – Luke Schwirtz

Luke Schwirtz is a Project Engineer at HaFSBX. He has a strong track record of implementing cost-effective automation solutions and leading process improvements that enhance performance, increase efficiency, and support overall quality across projects.

Is your Hopper Burping?

Manufacturing Powder Substance and output from machine. Powder Material Handling Equipment.
by Caleb Meyer
In many powder handling systems, performance challenges don’t originate from a single piece of equipment. Instead, they develop across the full process—where air movement, material flow, and equipment design intersect.
This is especially true in systems that feed packaging operations. When air is not properly controlled, even a well-designed process can struggle. The result is inconsistent flow, material loss, sanitation concerns, and operational inefficiencies.

Air Imbalance and Material “Burping”

A common issue in powder transfer systems is the uncontrolled release of air from hoppers during filling or discharge.

As powder enters a hopper, displaced air must escape. If it cannot, pressure builds. Eventually, the system releases that pressure suddenly – forcing air and product back out of the inlet.

Operators often describe this as “burping.”

In this condition:
  • Product is pushed back up through the inlet
  • Dust and fines escape into the surrounding environment
  • Temporary solutions (like socks or containment bags) fill repeatedly with material
  • Cleaning requirements increase, and processing consistency suffers

This is not just a nuisance. It impacts throughput, sanitation, and overall system reliability.

Additionally, worn or undersized airlocks can allow leakage, further disrupting pressure balance within the system.

Addressing Airflow and System Performance

One effective way to resolve these types of material handling issues is by addressing airflow first, then optimizing the surrounding equipment as needed.

Rather than immediately replacing large portions of the system, the process should begin by stabilizing air movement. Once airflow is properly controlled, it becomes easier to identify other inefficiencies and make targeted improvements that support consistent operation.

1. Pressure Relief Through Bin Venting

The first step is to provide a controlled path for air to escape.
Bin vents or compact filter receivers can be installed at key inlet points to:
  • Capture displaced air during filling
  • Prevent pressure buildup inside the vessel
  • Retain product while allowing clean air discharge
By regulating airflow at the source, the system becomes more stable and predictable.

2. Sealing Systems with Upgraded Airlocks

Airlocks are essential for maintaining proper pressure boundaries between equipment.
Upgrading to quick-clean airlocks provides key advantages:
  • Improved sealing to reduce air leakage
  • Easier access for inspection and cleaning
  • Reduced maintenance complexity

In many cases, simplifying maintenance procedures directly supports better system uptime and sanitation practices.

Together, these changes address immediate airflow issues while laying the groundwork for further system improvements.

Rethinking Powder Hopper Design

Existing industrial hopper design can limit performance. Older layouts often lack:

  • Adequate clean-out access
  • Proper geometry to support consistent flow
  • Structural capacity for upgraded downstream equipment

Designing for Real-World Performance

In many facilities, hoppers are expected to do more than simply hold material. They must support consistent flow, integrate with surrounding equipment, and allow for efficient cleaning between production runs.

Effective industrial hopper design typically focuses on a few key areas:

Flow Performance

  • Steeper cone angles can help promote consistent discharge
  • Smooth internal surfaces provide a key hopper bridging solution by reducing material buildup and promoting consistent flow

Structural Considerations

  • Reinforced outlet connections help support the weight of modern airlocks and downstream equipment
  • Proper structural support helps prevent long-term wear or misalignment

Cleanability and Accessibility

  • Multiple access points improve operator reach
  • Thoughtful door placement minimizes areas where material can collect
  • Designs that reduce ledges or flat surfaces help prevent buildup
These features are especially important in applications where sanitation and changeover speed directly impact production efficiency.

Working Within Existing Systems

Most upgrades take place within operating facilities.

This means new equipment must often integrate with:

  • Existing packaging or processing equipment
  • Fixed connection points or elevations
  • Limited installation access

In these environments, success depends on designing equipment that fits the process as it currently exists—not just how it would ideally be arranged.

Accounting for these real-world constraints early helps reduce installation challenges and ensures a smoother integration.

The Result: System Changes that Support A More Stable and Flexible Process

When airflow is properly controlled and equipment is designed with both performance and maintenance in mind, improvements are seen across the entire operation.

More Consistent Material Flow

Reducing pressure imbalances helps eliminate surging or backflow, leading to smoother, more reliable operation

Improved Sanitation and Changeover

Accessible designs and quick-clean components make it easier to clean equipment and switch between products.

Reduced Maintenance Burden

Equipment that is easier to inspect and service helps minimize downtime and simplifies routine maintenance tasks.

Better System Integration

Designing components to work together can help improve reliability and reduce issues during installation and operation.

Key Takeaways for Engineers and Operators

Many common powder handling challenges — including material loss, inconsistent flow, and bridging — call for hopper bridging solutions rooted in airflow control and equipment design.

Addressing these issues typically involves:

  • Managing air movement within the system
  • Ensuring proper sealing at key transition points
  • Designing equipment for accessibility and cleanability
  • Accounting for real-world installation and integration constraints
When these factors are considered together, the result is a system that not only resolves immediate problems, but is also easier to operate, maintain, and adapt over time.

About HaFSBX
HaFSBX has over 50 years of providing proven solutions to dry and liquid ingredient handling challenges.

We design turnkey systems for projects of all sizes. Our team understands our customers’ concerns and takes the time to listen, develop a plan, and communicate along the way. If you need someone you can trust and want to eliminate the stress of managing the details of your next project, contact us today to discuss your next project and how our team can help.

About the Author – Caleb Meyer

Caleb Meyer, a chemical engineer from the University of Minnesota, brings a strong technical foundation and a practical approach to delivering effective solutions in the ingredient handling industry. With experience spanning both engineering and customer-focused roles, he supports projects with a focus on performance, quality, and real-world application.

Adding Capacity Without Disrupting Your Process: A Practical Approach to Bulk Bag Unloading

by Nick Smith
In many food and ingredient processing facilities, capacity needs don’t change overnight—but when they do, it’s critical to be ready.

Expansions, new production lines, or increased throughput targets often require upgrades to a bulk bag handling system. But adding capacity isn’t always about redesigning a system from scratch. In many cases, the most effective solution is to build on what already works.

The Challenge: Scaling an Existing Process

When a bulk bag unloading system is already proven in operation, adding capacity introduces a different kind of challenge.

Instead of solving a new process issue, the focus shifts to:
  • Increasing throughput without disrupting current operations
  • Integrating additional equipment into an existing layout
  • Maintaining consistency across operators, processes, and downstream systems
For ingredients like maltodextrin—commonly handled in bulk bags and conveyed pneumatically—reliability and consistency are key. Any new equipment must match the performance of the existing system while fitting cleanly into the established process.

The Solution: Replicating a Proven System

One of the most effective ways to expand capacity is by replicating a system that operators already trust.

Rather than introducing new bulk bag handling system configurations, a duplicate unloader can:

  • Maintain familiar operation for plant personnel
  • Reduce risk during installation and startup
  • Ensure consistent material handling performance
Bulk bag unloaders can sometimes be installed in parallel with an existing unit, allowing both systems to feed the same downstream conveying line. This can give operators the flexibility to run one or both units depending on production demand.

Designing for Integration

Even when duplicating equipment, integration details matter.

Adjustments can be made to accommodate additional inline components — such as a magnet and metal detection equipment — within the overall bulk bag unloading system layout. Instead of leaving those modifications to the field, supporting structures can be designed to allow those components to be installed directly into the stack-up.

These types of small design considerations can:

  • Simplify installation
  • Reduce field modification time
  • Improve overall system reliability
At the same time, optional features—such as bag conditioning equipment—can be designed into the system without being immediately installed. This allows for future upgrades without requiring major redesigns.

The Result: Flexible Capacity for Future Demand

Expanding bulk bag unloading capacity with a duplicate unloader can allow for system flexibility without adding complexity.

Operators can:
  • Run a single unit during normal production
  • Bring a second unit online as demand increases
  • Maintain consistent performance across both systems
This type of approach supports growth while minimizing disruption to existing processes.

Key Takeaways

When expanding capacity in a bulk bag unloading system, a few principles stand out:

  • Proven designs are often the most reliable starting point
  • Duplication can be more effective than redesign
  • Planning for integration reduces installation challenges
  • Designing for future flexibility adds long-term value
  • Operator interaction plays a key role in system reliability

In many cases, simple, well-executed solutions deliver the greatest impact—especially when they’re built on systems that already work.

At HaF, we help manufacturers scale their processes by building on what already works—whether that means replicating proven bulk bag handling systems, designing for seamless integration, or preparing equipment for future capacity needs. Our focus is on practical, real-world solutions that support reliable operation today while giving you the flexibility to grow as demand changes.

About HaFSBX
HaFSBX has over 50 years of providing proven solutions to dry and liquid ingredient handling challenges.

We design turnkey systems for projects of all sizes. Our team understands our customers’ concerns and takes the time to listen, develop a plan, and communicate along the way. If you need someone you can trust and want to eliminate the stress of managing the details of your next project, contact us today to discuss your next project and how our team can help.

About the Author – Nick Smith

Nick Smith, a Mechanical Engineer, brings a versatile engineering background with experience across multiple industries, including manufacturing and system design. With a focus on delivering practical, results-driven solutions, he has contributed to projects ranging from equipment and system development to process improvements, supporting efficient execution and reliable system performance throughout each project.

Small Upgrades, Big Impact: Enhancing Wet Dust Collector Performance in a Dairy Facility

photo of various dairy products including cheese, milk and eggs. Wet Dust Collector Performance Article - HaFSBX Equipment
by Ben Kozmik

In dairy and food manufacturing environments, dust collection equipment does far more than manage airborne particulates. It supports plant safety, sanitation, and operator efficiency — all while operating continuously in demanding conditions. While an industrial dust collection system is often built for long service life, strategic upgrades can deliver meaningful improvements without requiring a full replacement.

When a dairy manufacturer partnered with HaF to review an existing wet dust collector installation, the objective was clear: improve day-to-day operation and maintenance while maintaining the integrity of the existing industrial dust collector system. By focusing on airflow control and creating a design with routine maintenance handling in mind, HaF delivered targeted enhancements that had a positive impact on performance, cleanability, and usability.

photo of various dairy products including cheese, milk and eggs. Wet Dust Collector Performance Article - HaFSBX Equipment

Evaluating an Existing Wet Dust Collection System

The facility relied on a wet dust collector to capture airborne dust. Over time, operators identified challenges that affected both system efficiency and routine maintenance.

Airflow balancing on the second floor of the system was limited, making it difficult to fine-tune performance as operating conditions changed. In addition, the existing mist eliminators were heavy and difficult to handle, making cleaning time and physical strain a concern during maintenance. While the system continued to function as designed, these factors created opportunities for improvement.

Rather than pursuing a complete system replacement, the team focused on practical, application-driven upgrades that could be integrated into the existing footprint.

Engineering Targeted Improvements for Performance and Cleanability

HaF engineers collaborated closely with the customer to develop solutions that addressed both technical requirements and operator feedback.

To improve airflow control, HaF designed and supplied a custom stainless steel manual damper valve. The damper allowed for precise airflow balancing while maintaining compatibility with the existing duct configuration. Sanitary ferrules and removable tubing were incorporated to support sanitation and inspection practices typical in food processing environments.

Mist eliminator upgrades were designed with sanitation, ergonomics, and ease of maintenance in mind. HaF engineered 304 stainless steel mist eliminators sized to fit directly into the existing housing. The new configuration emphasized lightweight construction and simplified handling. It was designed with routine handling maintenance in mind. Integrated handles and identification markings improved usability, while the solid, smooth construction minimized cracks and crevices that could compromise cleanability.

Designed to Fit Existing Equipment and Food-Grade Standards

One of the engineering challenges was ensuring the upgraded mist eliminators would integrate seamlessly into the existing housing. Precise measurements, close coordination between engineering and fabrication teams, and application-specific design adjustments were critical to achieving a proper fit.

By designing the upgrades around the existing structure, HaF was able to minimize downtime and avoid disruptive modifications—an important consideration in active dairy production environments where uptime and sanitation are critical.

Incremental Upgrades with Meaningful Result

This project demonstrates how thoughtfully engineered upgrades can extend the value of an existing industrial dust collection system. By improving airflow control and simplifying routine maintenance, the industrial dust collector system became easier to operate and clean. This aligns with the needs of a modern dairy facility.

For food and dairy manufacturers looking to enhance system performance without major capital investment, targeted improvements to wet dust collection equipment can deliver measurable operational benefits. With application-driven engineering and a clear focus on operator experience, even small upgrades can make a big impact.

This case example is shared for informational purposes only. System performance, maintenance needs, and outcomes vary based on application, operating conditions, and system design. No results or regulatory compliance are guaranteed.

About HaFSBX
HaFSBX has over 50 years of providing proven solutions to dry and liquid ingredient handling challenges.

We design turnkey systems for projects of all sizes. Our team understands our customers’ concerns and takes the time to listen, develop a plan, and communicate along the way. If you need someone you can trust and want to eliminate the stress of managing the details of your next project, contact us today to discuss your next project and how our team can help.

About the Author – Ben Kozmik

Ben Kozmik is a project engineer and has been in the ingredient handling industry for 30 years. His experience and passion for customer’s success has made him a trusted partner for many of HaFSBX’s clients. 

Whey Protein Rehydration: Achieving Complete Wetting, Dispersion, and Functional Performance

Measuring cup filled with whey protein powder on a dark surface
by Gonzalo Garcia

Whey protein powders are widely used in dairy beverages, nutritional formulations, cultured products, and recombined dairy applications. While whey proteins are inherently soluble, rehydration remains one of the most critical—and often problematic—steps in processing. Incomplete wetting, whey protein clumping, entrained air, and inconsistent dispersion can compromise product quality, protein functionality, and downstream processing efficiency.

HaFSBX designs specialized dry-liquid mixing and slurry technologies designed to address these challenges by controlling how whey protein powders are introduced, wetted, and dispersed into liquid streams.

Measuring cup filled with whey protein powder on a dark surface

HaFSBX Understands Whey Protein Rehydration Challenges

Rehydration of whey protein is more than simple dissolution. For powders to be successfully reconstituted, they must:
  • Be rapidly and uniformly wetted upon contact with liquid
  • Disperse without agglomeration or clumping
  • Hydrate fully without excessive shear or residence time
  • Minimize air entrainment and foam formation
Conventional batch mixing often struggles with whey protein powders due to surface tension effects, fine particle size, and trapped air. These issues commonly lead to undispersed “fish eyes,” unstable slurries, and longer processing times.

Single-Pass Whey Protein Rehydration Using the VACUCAM® Process

HaFSBX’s approach to whey protein rehydration centers on the VACUCAM® Ejector Mixer, an in-line whey protein mixing system designed for instantaneous wetting and dispersion.

Rather than adding whey protein directly into an agitated tank, the VACUCAM® process introduces conditioned dry powder and liquid in two independent, highly controlled streams. A high-velocity liquid jet creates a vacuum that conveys the powder into the mixing zone, where both phases are atomized before contact.

This design maximizes the exposed surface area of both liquid and powder at the moment of interaction, producing:

  • Rapid and uniform wetting
  • Consistent dispersion without agglomeration
  • Immediate hydration suitable for downstream use

HaFSBX’s focus on its milk powder reconstitution systems—including those handling whey protein powders—are capable of complete rehydration in a single pass, eliminating the need for prolonged batch mixing or recirculation in many applications.

Temperature Control During Whey Protein Rehydration

One of the most significant challenges in whey protein mixing is controlling finished product temperature. Excessive heat can negatively impact protein functionality and increase fouling and energy consumption.

HaFSBX systems are designed to fully hydrate whey protein powders directly into cold water or cold milk, allowing the reconstituted liquid to be used immediately downstream without additional cooling steps.

This capability is especially important in:

  • Nutritional beverages
  • Dairy beverage bases
  • Cultured dairy products
  • High-protein formulations

Integrated Dry Handling for Whey Protein Powders

Rehydration performance depends not only on the mixer, but also on how machine whey protein is handled prior to wetting. HaFSBX integrates bulk bag discharge, surge hoppers, and controlled feed systems to ensure consistent and dust-free delivery of whey protein to the mixing process.

Design considerations include:

  • Maintaining consistent powder feed rates
  • Preventing segregation or flooding
  • Eliminating dust and operator exposure
  • Supporting automated, hands-free operation
These systems are designed as part of a total dry-liquid process, rather than as isolated pieces of equipment.

Sanitary Design and CIP Compatibility

Whey protein rehydration systems used in food and dairy applications must meet strict sanitary requirements.

HaFSBX’s milk powder and whey protein reconstitution processes are designed to USDA and 3-A standards, with clean-in-place (CIP) compatibility on both the dry and wet sides of the system.

This enables:
  • Reduced sanitation downtime
  • Improved food safety compliance
  • Repeatable batch-to-batch performance

Applications for Whey Protein Rehydration

HaFSBX whey protein rehydration solutions are applied across a wide range of dairy and beverage processes, including:
  • Dairy beverages
  • Nutritional and protein-fortified formulas
  • Cultured dairy products
  • Recombinant milk and dairy bases
  • Process cheese and frozen dessert mixes
Across these applications, the goal remains the same: consistent, fully hydrated whey protein without clumps, excess air, or extended processing time.

Conclusion

Effective whey protein rehydration is critical to product quality, processing efficiency, and operational consistency. The Vacucam addresses the fundamental challenges of wetting, dispersion, whey protein clumping, and hydration by combining engineered dry handling, high-efficiency in-line mixing, and sanitary system design into a single, integrated solution.

By focusing on how and when whey protein powders contact liquid—rather than relying on prolonged mechanical agitation—HaFSBX systems deliver rapid, repeatable rehydration and whey protein mixing aligned with modern dairy and beverage processing requirements.

About HaFSBX
HaFSBX has over 50 years of providing proven solutions to dry and liquid ingredient handling challenges.

We design turnkey systems for projects of all sizes. Our team understands our customers’ concerns and takes the time to listen, develop a plan, and communicate along the way. If you need someone you can trust and want to eliminate the stress of managing the details of your next project, contact us today to discuss your next project and how our team can help.

About the Author – Gonzalo Garcia

Gonzalo Garcia, a chemical engineer from the University of Minnesota, has become a trusted partner in the ingredient handling industry over the years. He is committed to helping customers navigate challenges and provide solutions that bring success. 

Engineering Challenges of Natural Color Handling in Food and Beverage Systems

Vibrant Natural Color Food Ingredients in individual stacks, including paprika, turmeric, and other spice powders. HaFSBX Natural Color Handling in Food and Beverage Manufacturing.

by Mitch Lund

As food and beverage manufacturers move toward cleaner labels and more natural formulations, natural colors present a new set of challenges inside the plant. Derived from fruits, vegetables, spices, and other raw materials, these colors are often sensitive to heat, light, shear, and oxygen, making proper ingredient handling just as critical as the color itself. From receiving and storage to conveying, batching, and mixing, the way natural colors are handled can directly impact consistency, vibrancy, and product quality.

Common Natural Color Ingredients

Paprika • Annatto • Beet & Vegetable Powders • Turmeric • Spirulina • Caramel Colors • Fruit & Vegetable Juice Powders. Often these ingredients can be supplied from paper bags, bag in drums/boxes, bulk bags, or bulk systems and integrated with automated ingredient handling.

Sanitary, Food Focused System Design

Natural color ingredients present unique challenges due to sensitivity to heat, shear, and incomplete wetting. Even minor variations in dispersion can affect shade consistency, product appearance, and overall batch quality. Processors also need equipment that supports sanitary operation while minimizing dust using a dust collector system, waste, and manual handling. HaFSBX addresses these challenges with the VACUCAM® Ejector Mixer, delivering fast, consistent, and gentle dispersion of natural coloring powders in sanitary, closed systems.

Natural Coloring Challenges

  • Incomplete wetting, fisheyes, and floating pigments

  • Shade variation and batch‑to‑batch inconsistency

  • Pigment degradation from heat or mechanical shear

  • Long batch times and high labor requirements

  • Dusting, sanitation risks, and yield loss

VACUCAM® Technology Overview

The VACUCAM® Ejector Mixer conveys dry color powders into a near‑perfect vacuum created by a high‑velocity liquid stream. The system immediately wets the powder, preventing agglomerates and ensuring uniform, shear-free dispersion. Systems are supplied as skidded VACUCAM® units for single‑pass, batch, or recirculation processing. 

Why Natural Color Ingredient Processors Choose VACUCAM®

QUALITY

  • Uniform dispersion with no streak or fisheyes

  • Excellent batch‑to‑batch color repeatability

  • Cold, low‑shear dispersion protects sensitive pigments

CAPACITY

  • Rapid powder incorporation minimizes batch times

  • High‑capacity systems support scale‑up

  • Enables parallel processing vs. sequential addition

OPERABILITY

  • Closed, dust‑free induction

  • Full CIP compatibility on dry and wet sides

  • Low maintenance—pump is the only moving part
  • Low energy and labor requirements

Expand Your Color Processing Capabilities

By approaching natural colors as both a sensitive ingredient and a process variable, manufacturers can achieve consistent visual performance while maintaining efficiency, quality, and confidence in clean‑label production. The VACUCAM® Ejector Mixer is a key differentiator for HāFSBX in natural color applications—delivering consistent color quality, improved yields, and efficient production while meeting food‑grade sanitary expectations. 

About HaFSBX
HaFSBX has over 50 years of providing proven solutions to dry and liquid ingredient handling challenges.

We design turnkey systems for projects of all sizes. Our team understands our customers’ concerns and takes the time to listen, develop a plan, and communicate along the way. If you need someone you can trust and want to eliminate the stress of managing the details of your next project, contact us today to discuss your next project and how our team can help.

About The Author – Mitch Lund
Mitch has been with HaF Equipment for more than 4 years and leads business development for HaFSBX in the baking and snack sectors. He has been in ingredient handling for 14 years and can be found at many of the industry trade associations HaF actively supports, including ABA, BEMA, and ASB. Mitch is a graduate of the University of Minnesota’s Chemical Engineering program and is passionate about helping customers grow and improve their businesses.