
Cocoa powder presents challenges in bulk material handling due to its variable fat content, poor flow characteristics, and sensitivity to moisture. In periods of supply chain volatility, manufacturers increasingly rely on surge storage systems to decouple procurement from production and improve operational resilience. This article explores the engineering considerations behind a surge bin system designed for cocoa handling, with a focus on flow reliability, space constraints, and hygienic design.
Cocoa Handling Challenges in Modern Manufacturing
- Poor flowability, particularly at higher fat contents
- Tendency to pack, bridge, or rat-hole in static hoppers
- Dust generation, requiring appropriate containment and filtration
- Strict hygienic requirements, especially in food-grade environments
Engineering Objectives for Cocoa Surge Storage
When designing a surge storage system for cocoa, several core objectives typically guide the engineering process:
- Increased surge capacity to buffer upstream supply variability
- Reliable discharge despite challenging material properties
- Minimal facility impact, particularly in retrofit installations
- Compatibility with existing conveying systems
- Food-grade construction and maintainability
Meeting these objectives simultaneously often necessitates a custom-engineered solution rather than an off–the–shelf bin.
Surge Bin Design Considerations
Storage Geometry and Construction
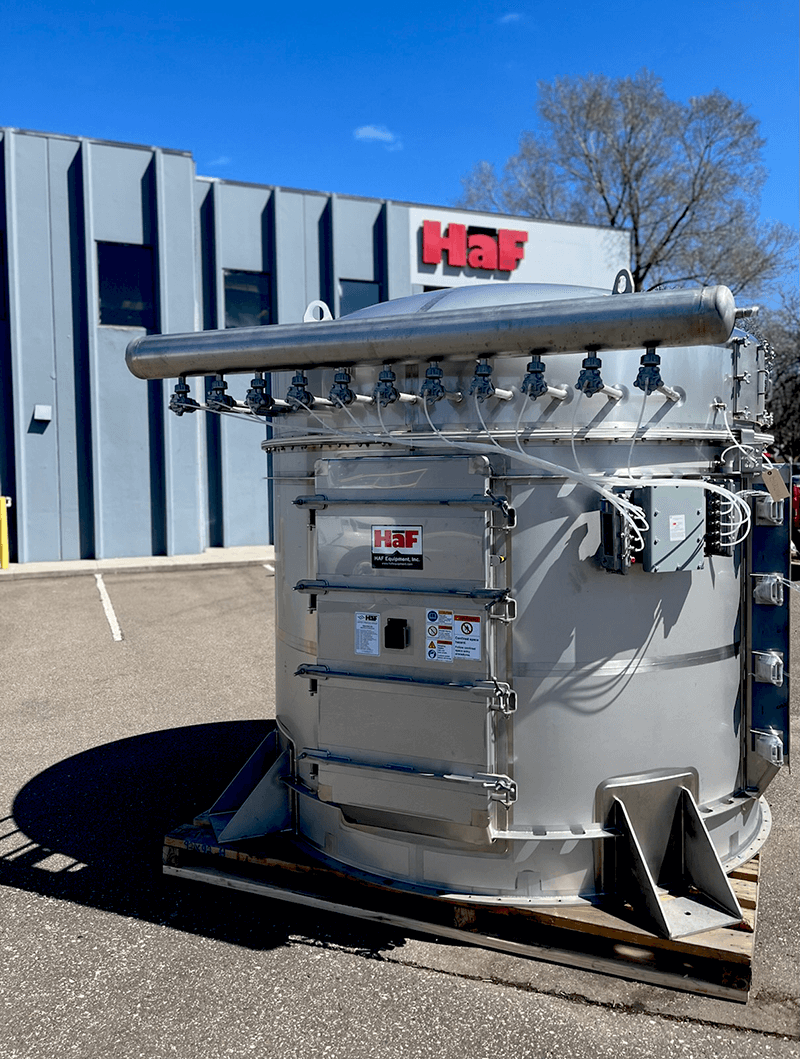
HaF designs surge bins to maximize usable storage volume within a constrained footprint. Cylindrical stainless steel construction is commonly selected for food applications due to its cleanability, corrosion resistance, and durability. Bin height and diameter are optimized to balance capacity, headroom limitations, and downstream feeding requirements.
Select the Correct Discharge
Every application is different. Cocoa’s flow behavior makes gravity discharge unreliable in most cases. To address this, HaF spends time reviewing space constraints, and what is upstream and downstream of the surge bin, to select the correct discharge method out of the surge bin so that the discharge system:
- Prevents material compaction
- Promotes first–in, first–out (FIFO) flow
- Reduces bridging and ratholing
- Improves consistency at the feeder inlet
HaF has several methods to promote cocoa flow out of a surge bin. Selecting the correct discharge method is particularly critical for powders with variable fat content.
Metered Feeding
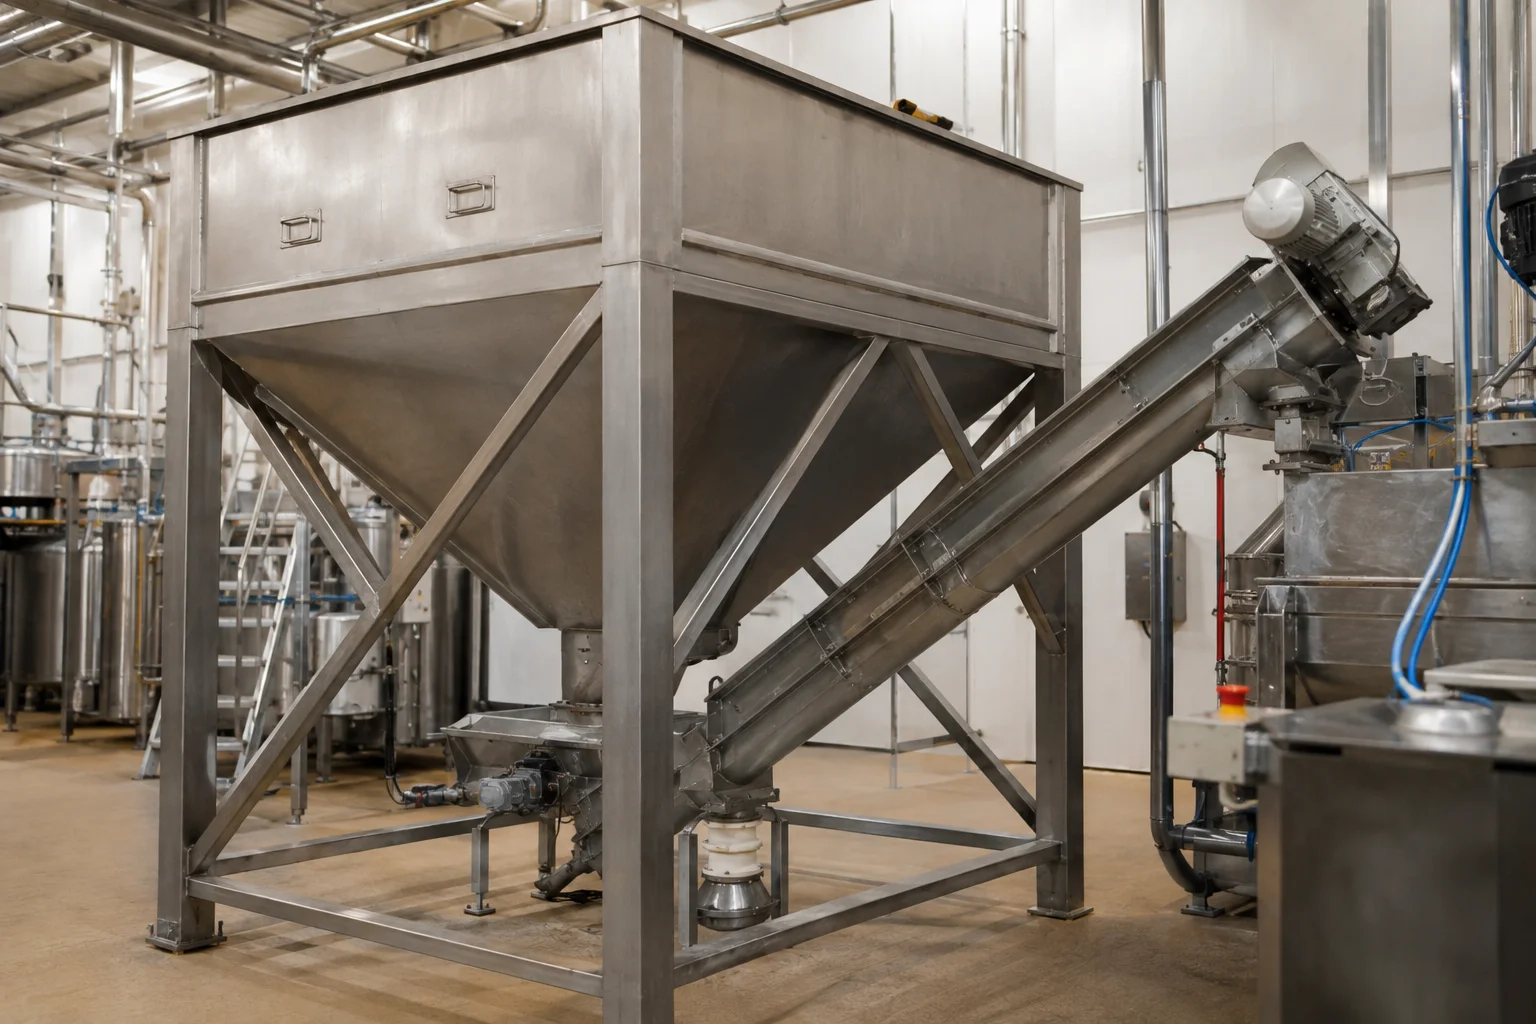
Downstream of the bin activator, an inclined screw feeder can be used to meter cocoa into the conveying or processing system. Screw feeders provide:
- Controlled, repeatable feed rates
- Positive material movement independent of head pressure
- Isolation between storage and process demand
Inclination and screw geometry are selected based on throughput requirements and bulk density.
Dust Control and Air Management
Cocoa powder is inherently dusty, making air management an essential component of surge bin design. A bin vent dust collector is typically mounted on the bin to:
- Allow displaced air to escape during filling
- Prevent dust migration into the surrounding environment
- Maintain negative pressure balance during discharge
Design features such as tool–free filter access and integrated silencers support both maintenance efficiency and operator comfort.
Material Properties Driving Design Decisions
Understanding cocoa’s physical characteristics is critical to a successful system design:
- Bulk density: Commonly in the range of 20–30 lb/ft³, depending on processing and fat content
- Fat content: Can exceed 20%, contributing to cohesion and smearing
- Moisture sensitivity: Excess moisture increases clumping and flow resistance
- Flow behavior: Classified as cohesive, requiring mechanical assistance for discharge
These properties justify the use of the correct discharge devices, controlled feeding, and sealed, hygienic construction.
Overcoming Space and Integration Constraints
In retrofit installations, physical space often becomes the primary constraint. Achieving meaningful surge capacity without building modifications requires close coordination between process engineering and mechanical design. Custom bin proportions, tailored support structures, and flexible inlet configurations allow the system to integrate with existing bulk bag unloaders, truck unloading stations, or conveyors.
Equally important is compatibility with upstream and downstream equipment. Designing standardized interfaces simplifies installation and reduces commissioning risk, particularly in facilities with mixed legacy and new equipment.
Key Engineering Takeaways
- Material-specific design is essential: Cocoa’s flow challenges cannot be addressed with generic storage solutions.
- Selecting the correct discharge method can improve reliability: Significantly reduce downtime associated with bridging and poor flow.
- Custom geometry maximizes value: Tailored dimensions enable higher capacity without structural changes.
- Operator-focused features matter: Easy access, cleanability, and low-maintenance components can improve long-term system performance.
Conclusion
Surge bins play a critical role in stabilizing production when handling challenging powders such as cocoa. By combining custom geometry, discharge technology, controlled feeding, and hygienic design, manufacturers can significantly improve both process reliability and supply chain flexibility. Thoughtful engineering—grounded in material science and practical constraints—remains the key to successful bulk ingredient handling. Contact HaF if you need help handling challenging powders!
About HaFSBX
HaFSBX has over 50 years of providing proven solutions to dry and liquid ingredient handling challenges.
We design turnkey systems for projects of all sizes. Our team understands our customers’ concerns and takes the time to listen, develop a plan, and communicate along the way. If you need someone you can trust and want to eliminate the stress of managing the details of your next project, contact us today to discuss your next project and how our team can help.
About the Author – Sam Edgerton
Sam Edgerton, a mechanical engineer from Purdue University, brings a strong engineering foundation and a practical, solutions-focused approach to the ingredient handling industry. With experience supporting engineered systems and project execution, he contributes to delivering efficient, reliable solutions that align with performance and quality goals.